A quart bottle forgives you. A tote does not.
The container arrives by forklift, not by conveyor. A driver sets a pallet down, and everything after that depends on whether it landed square and whether the opening is where the lance expects it. Half of a good tote filling system is container handling, not filling.
Tare weight is a moving target. IBC tare varies by manufacturer, pallet material, and valve configuration, and reconditioned totes add more spread. Assume a fixed tare, and you either give product away or ship short. That’s why both per-container tare (dynamic tare) and fixed tare are standard on our machines, selected and saved in each product’s recipe. More on tare weighing in net weight filling.
Density does not hold still. Temperature, batch variation, and solids content all move it. Anything that fills by volume and converts to weight needs recalibrating every time the product moves, which is why we fill on a scale. More on how net weight filling handles density changes.
Foaming decides the fill method. A non-foaming product tolerates a top fill. A foaming or solvent-based product usually needs the lance to fill subsurface, below the liquid level. That one decision changes the lance, the stroke, and the cycle.
High mix breaks rigid machines. Plants running totes, drums, and pails across dozens of SKUs cannot carry four dedicated machines and four sets of spares. That is a design problem, not a catalog problem.


We do not sell a standard tote filler off a spec sheet. Tote projects come to us as applications, scoped to the product, the containers, and the room.
Most of what we quote falls between a semi-automatic station and a conveyorized arrangement. Which one fits depends on your volume, your SKU count, and whether the product is one you would rather nobody stood over.
| Semi-automatic station | Conveyorized arrangement | |
| Container handling | Forklift sets the tote; the operator stages it and positions the lance | Chain-driven live roller or 2-strand drag chain conveyors move totes in and out; hands stay off the container |
| Best fit | Lower volume and a wide SKU mix | Higher volume, or products you would rather nobody stood over |
| Containers | Totes and drums, often on one station | Totes and drums, often on one station |
| Tare | Dynamic or fixed, set per product recipe | Dynamic or fixed, set per product recipe |
| Fill method | Top fill or subsurface, with diving lances up to an 80″ stroke | Top fill or subsurface, with diving lances up to an 80″ stroke |
Totes and drums on the same station. Most plants we talk to run drums one day and totes the next, off the same product line. In a lot of applications, one station handles both, which avoids a second capital request and a second set of spares. Running pails too? See our pail and semi-automatic filling machines.
This is the work we are known for. Products that stratify. Products with particulate. Products that behave differently at 8 am than at 4 pm. Containers nobody makes a standard machine for.
If two builders have already told you your application is not a fit, that is usually where we get interested. Start with our custom conveyor solutions page, or just call.


A short conversation starts a budgetary quote. We come back with one or more concepts and the pitfalls of each, not a push toward the biggest machine. On totes, that sometimes means a semi-automatic station rather than a conveyorized line.
Lance configuration, container range, fill method, and downstream equipment get written down. Deciding now whether drums or pails share the station is far cheaper than deciding later.
We build and integrate here, load your products as recipes, and run a factory acceptance test before shipping. On-site, we dial in setpoints against your real product, then you have parts, troubleshooting, and phone support.
We can work alongside your engineering and maintenance teams or run the project for you. Either way, we flag the risks early: operator safety around a container this size, maintenance access, and whether the line holds rate with forklift traffic in the cycle.


Full list on the industries we serve page.


"EGE Products is an Ag Chemical manufacturing company, and D&R Packaging has been an integral part of our success.
Working with D&R Packaging on our Dual Automated packaging lines is simple and cost effective with their full service program including design, installation, and on-going support.
The customer service at D&R Packaging is top tier. They are available whenever I call and can provide excellent assistance with repairs, trouble shooting, and part acquisition. D&R Packaging goes out of its way to provide a quality product and to keep it running."
Jedidiah B.
Alex P.
John F.
Jim C.
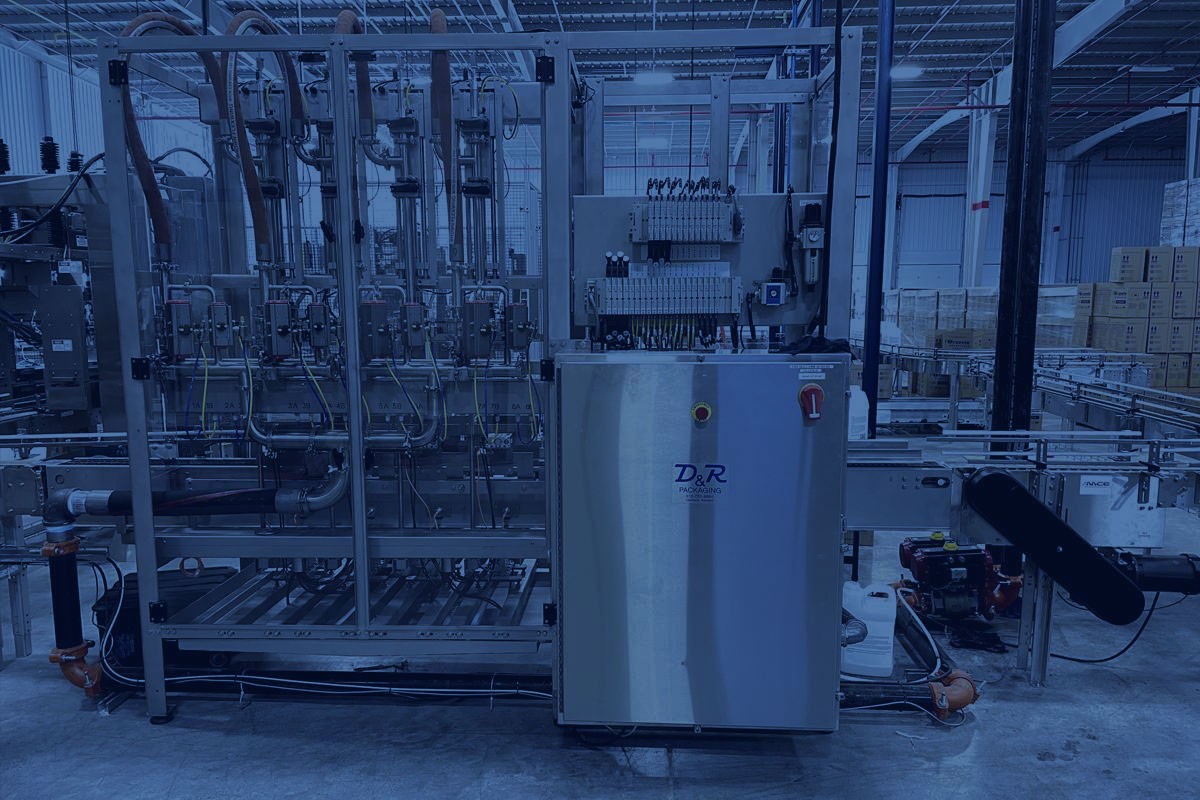
Tote filling equipment fills intermediate bulk containers, typically 275- and 330-gallon IBCs on their own pallet base. Most systems fill by weight, using a scale under the container and a lance that dispenses through the top opening.
We build tote fillers with diving lances up to an 80" stroke, which allows bottom-up filling of IBCs up to 550 gallons.
Fill time depends far more on your pump and line size than on the filling machine. In most plants, the real constraint is container handling: how quickly a forklift stages an empty and removes a full one.
Weight is the safer default, because density shifts with temperature and batch, and volumetric systems drift with it. Filling on a scale also gives you a defensible record of what went into each container.
In many applications, yes, and for most plants that is the right call. A station set up for both avoids a second machine and a second spare parts inventory.
Cost is driven by automation level, container handling, material compatibility, and how many SKUs the machine has to accommodate. A semi-automatic station and a fully conveyorized line are different orders of magnitude, so the honest answer starts with an application review.
If you sell the product by weight, plan for it up front. Our fillers are built with NTEP-certified load cells as standard, so your scale servicer can verify calibration and certify the filler as legal-for-trade.
Yes. Tare varies between manufacturers, pallet types, and reconditioned units, so our fillers can tare each container individually. Dynamic (per-container) tare and fixed tare are both standard, selected in each product's recipe.
Often, yes, including equipment other companies built. That can mean new controls, a different fill method, or tying an existing machine into a new layout.
We do. Our shop is in Merriam, Kansas, and we design, build, install, and support equipment for manufacturers across North America. Learn more about D&R.
Send us your product, your container specs, and your SKU list, and we will tell you honestly whether we are the right builder for the job. If your product is difficult, your mix is wide, or your density moves, that is the conversation we want to have.
Call (913) 722-6664 or request a quote to talk through custom tote filling equipment built for the way your plant actually runs.